Conveying unpacked food is a different engineering problem from conveying cases. The conveyor becomes part of the hygiene envelope, and construction that is perfectly adequate in a warehouse becomes a cleaning liability the moment product touches it.
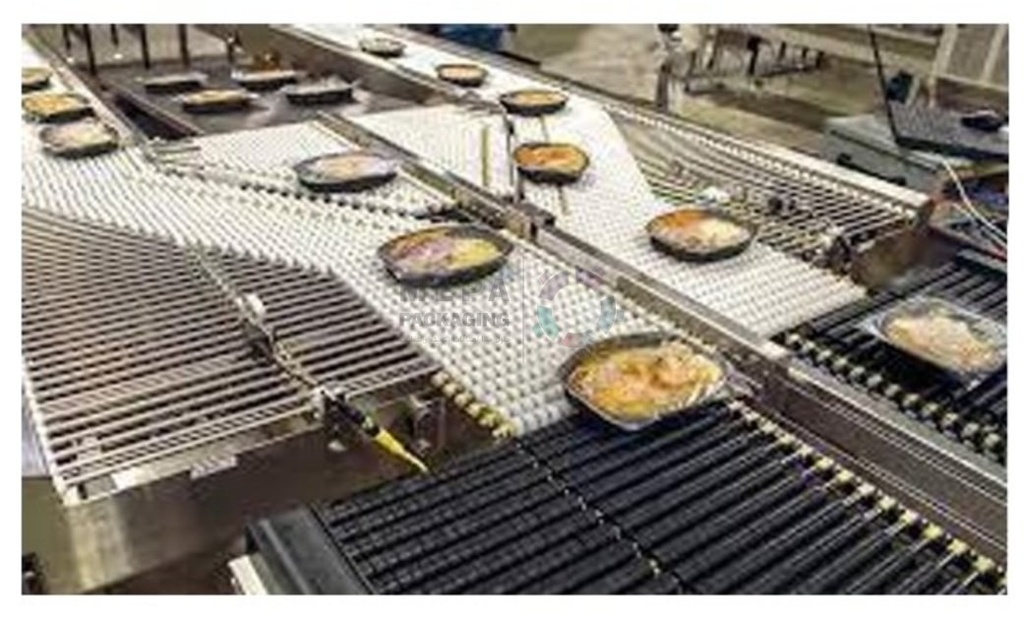
MEPA's food conveyor systems are built for that. Construction is possible in complete compliance with the strictest hygiene regulations and washdown requirements, and the systems are designed around the plant and the product rather than adapted from general-purpose parts. Where product is carried directly, FDA-compliant belt material and AISI 304 stainless steel construction are used.
The systems cover both bulk and packaged product, so one design language runs from the process end of the plant through to packed goods, with the same maintenance and cleaning regime across the line. Specification follows the plant: product characteristics, throughput, the cleaning chemistry and temperature the line is washed at, and the hygiene standard the site is audited against.
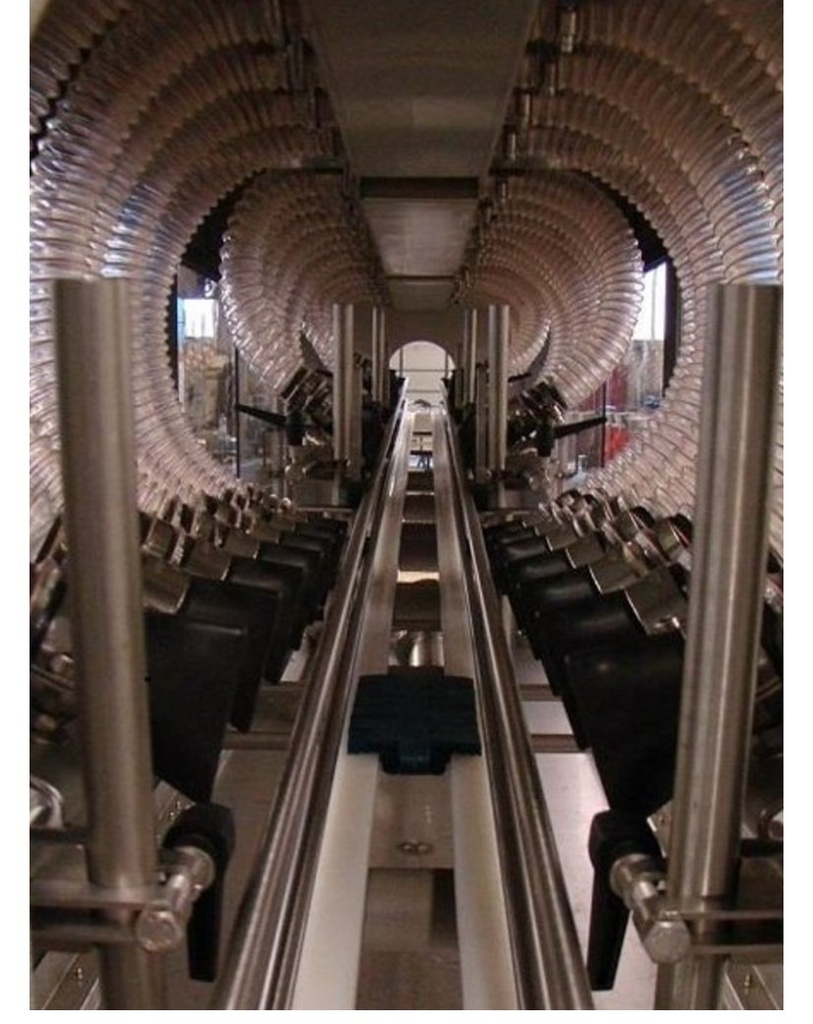
Hygienic conveyors for unpacked and packed food products, including spiral and elevating conveyors.
Food conveyors are designed for hygiene first: open frames, food-grade belts and easy cleaning.
Every conveying project starts from your layout, containers and target speeds.
- Stainless steel open-frame design
- Food-grade modular and wire belts
- Spiral conveyors for elevation and buffering
- Wash-down ready components
Request a quote